What's New in Solar PV Industry and SunEvo
News

New Products

  • What We Test Before a BESS Leaves the Factory? What We Test Before a BESS Leaves the Factory?
    Sep 14, 2026
    For utility, commercial and industrial (C&I) BESS buyers, factory testing is the most critical quality gate before shipment. A rigorous Factory Acceptance Test (FAT) program eliminates hidden defects, verifies full compliance with project specifications, and reduces on-site commissioning risks, operational failures and long-term maintenance costs. Every BESS we ship undergoes standardized, system-level testing covering safety, electrical performance, software communication and auxiliary systems to ensure plug-and-play reliability on site.   1. Visual & Mechanical Inspection We start with full mechanical verification to rule out production and assembly flaws. Our team inspects module appearance, cable routing, terminal tightening, cabinet sealing and structural integrity. We also verify IP rating compliance, door interlock functions and container structural stability. This step prevents loose connections, water ingress and mechanical failures that often cause intermittent on-site faults.   2. Core Electrical & Performance Testing This stage validates the BESS’s actual power and energy capability to match contracted parameters. We conduct full-rate charge and discharge cycling tests to verify usable capacity, system response speed and consistency across all battery modules. Cell voltage consistency and internal resistance testing eliminate module imbalance issues that degrade overall system efficiency and service life. We also test round-trip efficiency under rated operating conditions, ensuring DC efficiency ≥90% and AC efficiency ≥85% as standard benchmarks. All test data is recorded and archived for project handover and future operational reference.   3. Safety & Protection Functional Testing Safety is the top priority for BESS factory validation. We complete a full set of protection tests, including over-voltage, under-voltage, over-current, over-temperature and short-circuit protection. Insulation resistance (IR) and hipot tests are performed to detect insulation degradation, moisture intrusion and potential arcing risks, avoiding electrical hazards during long-term operation. Emergency shutdown (E-stop) and fault recovery testing is mandatory. We simulate real fault scenarios to confirm the system can cut off power stably without voltage spikes and restore normal operation safely after troubleshooting.   4. BMS & Communication System Verification A stable BMS and communication system is the foundation of intelligent BESS operation. We calibrate BMS firmware, verify real-time data collection of cell voltage, temperature, current and SOC accuracy. Meanwhile, we test seamless communication and data transmission between BMS, PCS, EMS and SCADA systems, ensuring compatible remote monitoring, data logging and remote control functions. All firmware versions, communication protocols and parameter settings are fully verified and fixed before delivery to avoid on-site debugging delays.   5. PCS S...
    View More
  • BESS Delivery Process: From Factory Integration to On-Site Commissioning BESS Delivery Process: From Factory Integration to On-Site Commissioning
    Sep 11, 2026
    For B2B buyers, delivering an overseas battery energy storage system involves more than shipping equipment. The PV system, batteries, PCS, BMS, EMS, protection devices, and monitoring platform must work together from factory testing through final commissioning. Our 5MW solar PV and 10MWh BESS project for a five-star hotel in Anguilla provides a practical example of this process.   1. Project Assessment and System Design The process starts with the customer’s electricity consumption, load profile, peak demand, grid conditions, available space, and operating objectives. For the Anguilla hotel, the solar-plus-storage system was designed to reduce reliance on expensive grid electricity. Engineers coordinated the PV capacity, battery capacity, PCS, EMS, transformers, switchgear, cooling, and fire-protection systems. For buyers, the key issue is clear responsibility: one party should manage the overall system design and equipment interfaces.   2. Factory Integration and Testing Before shipment, the main BESS components are assembled, configured, and tested where the system architecture allows. Typical factory checks include: · Battery rack and electrical connection inspection · BMS, PCS, and EMS communication · Charging and discharging functions · Cooling-system operation · Alarm and protection logic · Emergency-stop function · Remote monitoring · Start-up and shutdown sequences Factory acceptance testing helps identify compatibility and configuration problems before the equipment reaches an overseas site.   3. Packing and International Shipping Large BESS equipment must be protected against vibration, moisture, impact, and long-distance handling. During the Anguilla project, an EMS cabinet glass panel was damaged in transit. Because a suitable replacement was unavailable locally, it was replaced with acrylic, while the packaging was improved with full-surface cushioning and reinforced corner protection. This experience shows why buyers should review packaging based on the transport route and local replacement capabilities.   4. Site Preparation and Installation Before the equipment arrives, the site team should complete foundations, drainage, grounding, cable trenches, lifting access, auxiliary power, and communication infrastructure. After delivery, the equipment is inspected and installed. Work normally includes: · Equipment positioning · AC and DC cable connections · Grounding · Communication wiring · Cooling and fire-protection connections · Insulation and continuity testing For the Anguilla project, four SUNEVO technical team members provided on-site support for installation and system testing.   5. Commissioning and Handover Commissioning verifies that the complete system operates safely and according to the approved design. Testing typically covers: · BMS, PCS, and EMS communication · Battery charging an...
    View More
  • Five Risks When Sourcing PV and BESS Separately Five Risks When Sourcing PV and BESS Separately
    Sep 07, 2026
    For EPC contractors, project developers, and commercial energy users, buying solar PV equipment and battery energy storage systems from different suppliers can appear attractive. It allows more product choices and may reduce the initial purchase price. However, a lower equipment quotation does not always mean a lower total project cost. Once installation begins, the buyer may have to manage system compatibility, technical coordination, commissioning, warranties, and after-sales support across several companies. Before separating PV and BESS procurement, buyers should understand the following five risks.   1. The Equipment May Be Compatible on Paper—but Not in Practice A PV inverter, PCS, battery system, and EMS may each meet their own technical specifications, but that does not guarantee smooth system-level operation. Buyers may encounter problems such as: · Battery voltage not matching the PCS operating range · BMS and PCS communication failures · Unsupported CAN, Modbus, or Ethernet protocols · Charging and discharging limits that cannot be coordinated · EMS control logic that does not match the project’s operating strategy · Different firmware versions affecting communication The result may be frequent alarms, restricted battery output, incomplete state-of-charge data, or an inability to operate the system as designed. For buyers, the key question is not simply, “Are these products certified?” It is: “Have these exact models and software versions been tested together?”   2. No Single Supplier Takes Responsibility When a complete system comes from several suppliers, responsibility can become unclear when something goes wrong. The battery supplier may say the PCS settings are incorrect. The PCS supplier may blame the BMS communication. The EMS provider may argue that the required data is not being supplied correctly. Meanwhile, the buyer or EPC contractor must coordinate the investigation, arrange technical meetings, collect operating data, and manage the project delay. Before placing orders, buyers should define one responsible party for: · Overall system design · Communication integration · Parameter configuration · Protection coordination · Factory testing · On-site commissioning · Performance acceptance Without a clear responsibility matrix, the buyer may effectively become the system integrator.   3. Separate Warranties Do Not Equal a Complete System Warranty PV modules, inverters, batteries, PCS units, and EMS platforms normally have different warranty terms and operating conditions. A battery warranty may depend on: · Maximum charge and discharge current · Depth of discharge · Operating temperature · Annual energy throughput · Number of cycles · State-of-charge limits If another supplier’s equipment operates the battery outside these conditions, warran...
    View More
  • How Can a 261kWh C&I Battery Reduce Peak Demand Charges? How Can a 261kWh C&I Battery Reduce Peak Demand Charges?
    Sep 04, 2026
    How Can a 261kWh C&I Battery Energy Storage System Reduce Peak Demand Charges? For many commercial and industrial facilities, peak demand charges account for 30%–50% of total commercial and industrial (C&I) electricity bills for most factories, warehouses, and commercial facilities.  Electricity costs are determined not only by total energy consumption in kilowatt-hours (kWh), but also by the highest level of power drawn from the grid in kilowatts (kW). This peak demand may occur for only a short period, yet it can significantly increase the monthly electricity bill. A 261kWh commercial and industrial battery energy storage system can help reduce these charges through peak shaving.   What Are Peak Demand Charges? Peak demand charges are typically based on the highest average power demand recorded during a billing interval, often 15 or 30 minutes, within the billing period. For example, if several production lines, HVAC systems or EV chargers operate simultaneously, grid demand may rise sharply. Even if this peak lasts for only a short time, the facility may be billed according to that maximum demand level. Demand charges are measured in kW, while energy consumption is measured in kWh. This distinction is important when sizing a battery storage system.   How Does a 261kWh Battery Reduce Peak Demand? A C&I battery energy storage system continuously monitors the facility’s electricity demand through an energy management system. When grid demand approaches a predefined limit, the battery discharges to supply part of the load. This reduces the power drawn from the utility grid and helps prevent a new monthly demand peak. The operating process is straightforward: The battery charges during low-demand periods or from surplus solar generation. The energy management system monitors the facility’s load in real time. When demand exceeds the control threshold, the battery begins discharging. Grid demand remains below the target limit whenever sufficient battery power and stored energy are available. This process is known as peak shaving. The U.S. Department of Energy describes peak shaving as the use of energy storage to reduce peak power demand and avoid demand-related electricity charges. U.S. Department of Energy   Why Power and Energy Ratings Both Matter The 261kWh rating indicates how much energy the battery can store. However, peak-demand reduction also depends on the system’s power rating. For example, a 125kW/261kWh C&I battery system can theoretically supply up to 125kW of power while its available stored energy lasts, subject to operating limits, state of charge, conversion losses and reserve requirements. If a facility needs to reduce a 100kW peak for 90 minutes, the required discharge energy is approximately: 100kW × 1.5 hours = 150kWh A 261kWh system may be able to support this peak-shaving event if sufficient usable capacity is available. However, it cannot reduce a peak that exc...
    View More
  • Air Cooling vs Liquid Cooling for C&I Storage Air Cooling vs Liquid Cooling for C&I Storage
    Sep 03, 2026
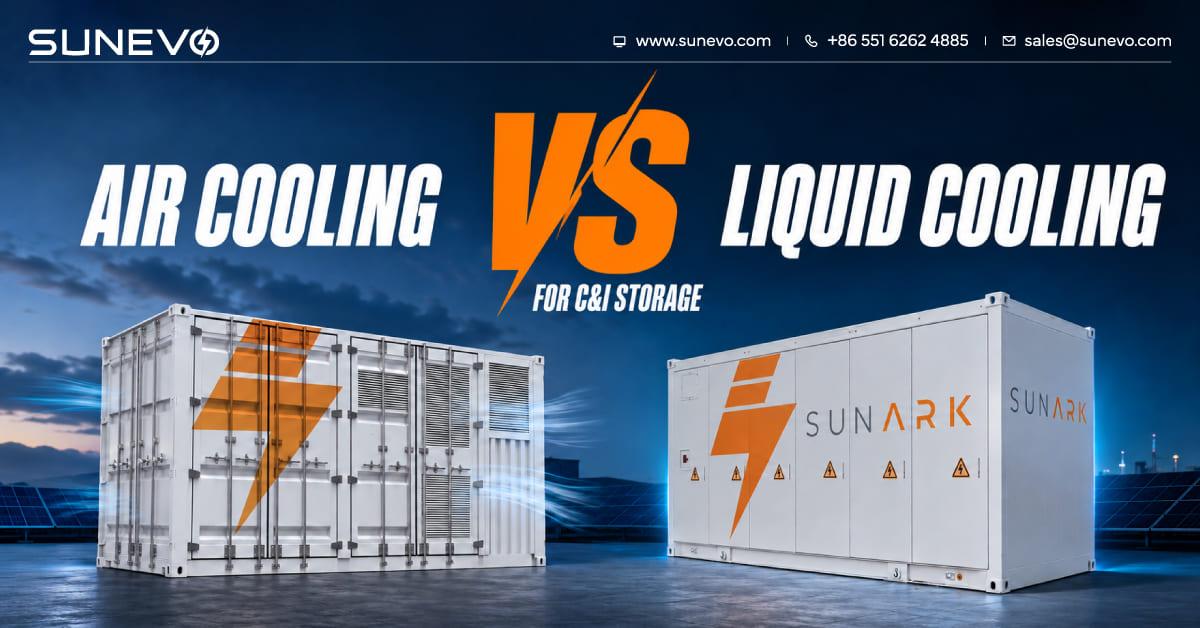
    Air Cooling vs Liquid Cooling for C&I Energy Storage: Which Thermal Management Is Right for Your Project Compare air-cooled and liquid-cooled C&I battery energy storage systems on temperature uniformity, CAPEX, O&M, footprint, and real-world scenarios to make the correct BESS selection.   Key Takeaways Thermal management directly determines C&I BESS safety, battery cycle life, auxiliary power consumption, and total-cost-of-ownership (TCO). Neither air cooling nor liquid cooling is universally superior.   Air-cooled C&I ESS: Lower upfront cost, simple maintenance; best for small-medium capacity, mild climate, low-moderate cycling duty cycle Liquid-cooled C&I ESS: Superior cell temperature uniformity, higher power density, strong environmental adaptability; ideal for large-scale, high-rate, frequent cycling or harsh climate projects.   How Air Cooling and Liquid Cooling Work for C&I BESS Air-Cooled System Air cooling uses fans and HVAC units to circulate air across battery module surfaces to dissipate heat. Core components include fans, filters, air ducts and air-conditioning units. No liquid circulation loop is required, with a simple mechanical structure and low engineering barrier. Under high load or high ambient temperature, air’s low thermal conductivity leads to uneven heat dissipation. Cell-to-cell temperature difference normally reaches 815℃, creating local hotspots that accelerate inconsistent battery degradation.   Liquid-Cooled System Liquid-cooled BESS adopts closed-loop glycol-water coolant circulating through cold plates tightly attached to battery modules. Heat is transferred to external heat exchangers and released to the ambient environment. Well-designed liquid cooling restricts cell-to-cell temperature delta within 2-3℃. A stable, uniform thermal field keeps lithium-ion cells operating inside the optimal 20-30 °C working window, slowing calendar- and cycle-based ageing significantly.   Side by Side Technical & Economic Comparison When to Choose Air-Cooled C&I Storage Select air cooling if your project matches most of the criteria below: 1. Small to medium capacity, generally ≤3 MWh; peak shaving, backup power with light to moderate cycling (once daily charge-discharge). 2. Mild ambient climate, no long term extreme high-temperature above 38-40 °C; clean air with low dust and salt mist. 3. Budget-sensitive CAPEX, limited local on-site maintenance resources. 4. Sufficient installation space to reserve airflow clearance for cabinets or containers. Typical use cases: small manufacturing workshops, commercial building backup power, small PV storage self-consumption projects.   When to Choose Liquid-Cooled C&I Storage Liquid cooling delivers better long-term return-on-investment for these conditions: 1. Large-capacity containerized C&I BESS ≥3 MWh, frequent daily cycling such as two charge, two discharge for demand response or arbitrage with...
    View More
  • Solar Wafer Prices Surge Up to 40% as Global Demand Rises Solar Wafer Prices Surge Up to 40% as Global Demand Rises
    Aug 24, 2026
    Solar wafer prices increased sharply across all major formats in the latest weekly market update released by the Silicon Industry Branch on August 20, 2026.   The average transaction prices for N-type monocrystalline wafers were: N-type G10L wafer (182 × 183.75 mm, 130 μm): approximately $0.165 per piece, up 40.00% week over week. N-type G12R wafer (182 × 210 mm, 130 μm): approximately $0.168 per piece, up 26.67% week over week. N-type G12 wafer (210 × 210 mm, 130 μm): approximately $0.180 per piece, up 10.91% week over week. Among the three formats, G10L wafers recorded the strongest increase.   Solar Cell and Module Prices Also Increase The price increase has extended further down the solar PV supply chain. Mainstream solar cell prices rose to approximately $0.049–$0.052/W, representing a 23.64% weekly increase. Mainstream solar module prices reached approximately $0.102–$0.105/W, up 1.45% from the previous week.   The smaller increase in module prices suggests that downstream manufacturers may still face resistance when passing higher material and cell costs on to project developers, distributors and EPC contractors.   What Is Driving the Solar Wafer Price Increase? According to the Silicon Industry Branch, the immediate driver is a sudden increase in downstream demand. Although domestic solar installation demand in China remains relatively stable, overseas solar cell manufacturers have accelerated wafer purchases amid concerns over potential trade risks related to the United States’ Section 232 tariff measures. This created a concentrated purchasing wave during the available policy window. At the same time, the arrival of India’s traditional solar installation season further strengthened export demand for Chinese solar wafers. The combination of rising orders, short-term supply constraints and buyer expectations of further price increases has pushed wafer prices significantly higher.   Why Did G10L Wafer Prices Rise Faster? The 182 mm G10L wafer format is primarily supplied to overseas markets, while G12R and G12 wafers are more closely linked to domestic Chinese demand. Because the latest demand increase was largely driven by export orders, G10L wafers experienced tighter availability and a much stronger price increase than the two larger formats.   Wafer Production Rates Remain Stable Despite the sharp rise in demand, the overall operating rate of China’s wafer industry remained broadly unchanged from the previous week: Two leading wafer manufacturers operated at approximately 52% and 54%. Vertically integrated manufacturers maintained operating rates of 56%–60%. Other wafer producers operated within a wider range of 50%–78%.   Production capacity has therefore remained relatively stable. In the short term, manufacturers may find it difficult to increase wafer supply quickly enough to fully meet the sudden rise in demand.   What Does...
    View More
  • U.S. Probes Solar Cell Tariff Evasion U.S. Probes Solar Cell Tariff Evasion
    Jul 22, 2026
    On July 13, 2026, in response to petitions filed by U.S. companies First Solar, Inc., Hanwha Q CELLS USA Inc., Talon PV, Swift Solar, Great Lakes Solex PR, LLC, DYCM Power, LLC, Suniva Inc., and Silfab Solar Inc., the United States initiated an anti-circumvention inquiry regarding crystalline silicon photovoltaic cells (whether or not assembled into modules) originating from China. The inquiry examines whether the following two types of circumvention of U.S. anti-dumping and countervailing duty orders are occurring: (1) Chinese-origin components are used to assemble photovoltaic cells and modules in Ethiopia, which are then exported to the United States; and (2) Chinese-origin components are used to assemble photovoltaic cells in Ethiopia, which are then exported to Vietnam for module assembly before being exported to the United States. This case covers products classified under U.S. Customs codes 8501.71.0000, 8501.72.1000, 8501.72.2000, 8501.72.3000, 8501.72.9000, 8501.80.1000, 8501.80.2000, 8501.80.3000, 8501.80.9000, 8507.20.8010, 8507.20.8031, 8507.20.8041, 8507.20.8061, 8507.20.8091, 8541.42.0010, and 8541.43.0010.On November 8, 2011, the U.S. Department of Commerce initiated anti-dumping and countervailing duty investigations into crystalline silicon photovoltaic cells (whether or not assembled into modules) originating from China. On October 17, 2012, the U.S. Department of Commerce issued final affirmative determinations in the anti-dumping and countervailing duty investigations concerning crystalline silicon photovoltaic cells from China. On November 1, 2017, the U.S. Department of Commerce initiated the first sunset reviews of the anti-dumping and countervailing duty orders on crystalline silicon photovoltaic cells from China. On March 9, 2018, the U.S. Department of Commerce issued a final affirmative determination in the first countervailing duty sunset review concerning crystalline silicon photovoltaic cells from China. On March 12, 2018, the U.S. Department of Commerce issued a final affirmative determination in the first anti-dumping sunset review concerning crystalline silicon photovoltaic cells from China. On February 1, 2024, the U.S. Department of Commerce initiated the second sunset reviews of the anti-dumping and countervailing duty orders on crystalline silicon photovoltaic cells from China. On June 6, 2024, the U.S. Department of Commerce issued a final determination in the second expedited anti-dumping sunset review concerning crystalline silicon photovoltaic cells from China. On June 7, 2024, the U.S. Department of Commerce issued a final determination in the second expedited countervailing duty sunset review concerning crystalline silicon photovoltaic cells from China.
    View More
  • Polysilicon Prices Continue to Slide! Polysilicon Prices Continue to Slide!
    Jul 20, 2026
    On July 8, the Silicon Industry Branch released this week's polysilicon prices. Compared to previous periods, the rate of price decline has slowed.The transaction price range for n-type recharge material (rod silicon) was 31,000–34,000 RMB/ton, with an average transaction price of 32,700 RMB/ton, down 0.30% week-on-week. The transaction price range for n-type granular silicon was 32,000–32,000 RMB/ton, with an average transaction price of 32,000 RMB/ton, down 0.93% week-on-week.According to the Silicon Industry Branch, the polysilicon market remains sluggish due to several factors: first, industry inventories continue to accumulate at high levels, while downstream procurement is limited to essential needs with little willingness to actively restock, resulting in subdued trading activity; second, some enterprises have been forced to adjust their shipment strategies to alleviate inventory pressure, and market behavior involving price concessions to boost sales volume has exerted downward pressure on prices. Driven by the combined effect of these factors, polysilicon transaction prices continued to edge lower within a low-price range this week. However, the magnitude of the price decline showed signs of narrowing significantly; this is primarily because current prices have largely reached the cash cost range for active producers across the industry, placing significant operational pressure on companies and limiting the scope for further price reductions.
    View More
  • US Stockpiles Lithium as Largest Mine Launches: Price Shakeup Ahead? US Stockpiles Lithium as Largest Mine Launches: Price Shakeup Ahead?
    Jul 17, 2026
    Lithium Included in Defense Stockpile for the First Time; US's Largest Lithium Mine Set to Launch—Is a Shift in Lithium Prices Coming?Critical minerals have evolved from mere commercial commodities into strategic resources, and the US strategy for stockpiling them is moving from policy planning to actual implementation.In February 2026, US President Trump announced the creation of a strategic critical mineral stockpile valued at $12 billion, aimed at boosting US industrial growth and reducing reliance on foreign trading partners. Dubbed "Project Vault," this initiative marks the first-ever critical mineral stockpile in US history, with Trump likening it to the nation's Strategic Petroleum Reserve.Trump emphasized that the stockpile's purpose is to foster industrial development; the US government has taken steps to ensure domestic access to all essential critical minerals and rare earths, highlighting investments in mining projects and the acceleration of federal permitting processes.In fact, lithium is not the first new-energy metal the US Defense Logistics Agency (DLA) has planned to acquire for strategic stockpiling. On August 19, 2025, the DLA announced plans to purchase 7,480 tons of cobalt; however, as cobalt prices surged 56% over the following two months and bidding companies could not commit to fixed prices for the next five years, the DLA was forced to cancel the cobalt procurement plan in October.Regarding lithium, the DLA had already issued a request for information in March concerning the potential purchase of 550 tons of lithium carbonate. Lithium's inclusion in the defense stockpile is inextricably linked to its strategic importance in the defense and energy sectors. From F-35 fighter jets to advanced chips, and from electric vehicles to grid-scale energy storage, lithium serves as a foundational material underpinning modern military and energy systems.After initiating plans to purchase lithium carbonate in March and conducting assessments throughout the second quarter, the DLA revised its strategy to a five-year plan to acquire 16,170 tons—a significant increase over the initial 550-ton target. The market had not anticipated US defense stockpiling of this nature; this move underscores the value of lithium carbonate as both a strategic and combat-readiness reserve. Regarding the market impact of the U.S. Department of Defense's lithium carbonate stockpile procurement plan: in terms of volume, the maximum amount is approximately 16,200 tons of lithium carbonate over five years—averaging about 3,200 tons of LCE (Lithium Carbonate Equivalent) annually—which breaks down to a monthly volume of just 200–300 tons. This scale is modest within the context of global lithium salt consumption and is significantly smaller than the market impact caused by demand fluctuations in the new energy vehicle and energy storage sectors.The author argues that this procurement should not be viewed as a source of incremental dem...
    View More
  • US Weighs Ban on Chinese Solar Inverter Imports US Weighs Ban on Chinese Solar Inverter Imports
    Jul 15, 2026
    On June 30, Reuters reported that the Trump administration is drafting a ban on the import of foreign inverters—devices used to connect solar projects and batteries to the power grid—amid concerns that China could use them to disrupt the power supply.
    View More
1 2 3 16
[  A total of  16  pages]
Top
Leave A Message
Leave A Message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.

Home

Products

Company

whatsapp